U.S. data center construction reached a seasonally adjusted annual rate of $50.7 billion in April 2026, according to Census Bureau construction spending data — the first time the category has cleared $50 billion, and about 28 percent above the same month a year earlier. Data centers now account for roughly half of all private office construction in the country.
Every one of those buildings is a copper distribution problem. That is why bus bar insulation taping has quietly become a volume process rather than a bench job.
Why bus bar volume scales faster than floor space
Rack densities keep climbing. Higher density means more current per row, and more current means bus bar and busway rather than cable. A single hyperscale hall can consume thousands of linear feet of bar, along with harnesses, tap-off connections, and switchgear interconnects.
The Department of Energy reports that data centers used about 4.4 percent of total U.S. electricity in 2023, with projections between 6.7 and 12 percent by 2028. Power at that scale does not travel on small conductors.
The taping step is still frequently manual
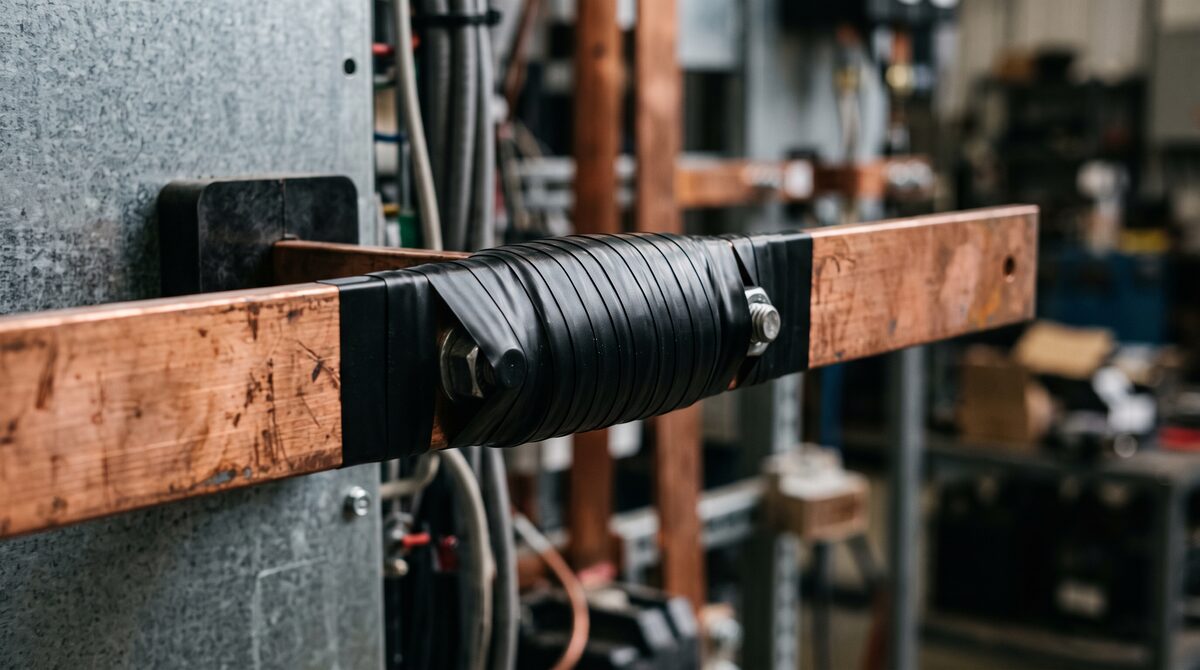
Bus bar insulation taping demands a controlled spiral overlap across the full length of the bar, with clean transitions at bends, joints, and breakouts. Done by hand, the process runs slowly and varies between operators. A thin spot is a dielectric problem. A heavy spot builds dimension that the enclosure clearance may not accept.
Fabricators handling this work face three recurring issues:
- Overlap drift across long runs, especially near the end of a shift
- Material change complexity, since polyimide, glass, and film composites all behave differently
- Breakout handling around tap points, where operators frequently stop and restart
Volume exposes all three. A shop taping fifty bars a month can manage by hand. A shop taping five hundred cannot.
Material choice complicates the job
Insulating tapes used on bus bar and harness work include polyimide, vinyl, foil, glass, mica, epoxy film, polyester, woven paper, reinforced filament, and fluorocarbon film composites. Each carries a different thickness, stretch, and tack. An overlap setting tuned for glass tape will not produce the same wrap in polyimide.
Automated taping heads hold a set overlap across all of those materials, because the head speed and the feed rate are controlled rather than judged. That matters most on repeat production, where a customer expects bar 400 to look like bar 4.
The same squeeze as the coil room
This is not an isolated trend. Coil shops are seeing rewind volume climb as new generation gets delayed, and both sides of the business are absorbing higher copper costs on every part they build. Rework on an insulated bus bar means stripping tape, inspecting the bar, and starting again — an expensive step at current material prices.
Shops handling growing bus bar volume are reaching the same conclusion coil shops reached: the process that sets the ceiling is the one worth automating first.
CAM Innovation: Custom Machinery for Motor and Coil Manufacturing
CAM Innovation builds custom automated machinery for the electric motor and coil manufacturing industry from Hanover, Pennsylvania. Every machine is Made in USA and designed around the process the customer actually runs.
Our Equipment Includes:
- Spiral Wrap Taping Machines — FT, RHT, CT, and ring taping systems for harnesses, coils, bus bars, and tubing
- Coil Manufacturing Equipment — Taping, forming, pressing, and winding systems for AC and DC form coils
Automating a process?
Contact CAM Innovation to discuss your part, your volume, and your shop layout.
Works Cited
- U.S. Census Bureau. “Construction Spending — Data.” U.S. Department of Commerce, 1 July 2026, https://www.census.gov/construction/c30/data/index.html.
- U.S. Department of Energy. “DOE Releases New Report Evaluating Increase in Electricity Demand from Data Centers.” Energy.gov, 20 Dec. 2024, https://www.energy.gov/articles/doe-releases-new-report-evaluating-increase-electricity-demand-data-centers.